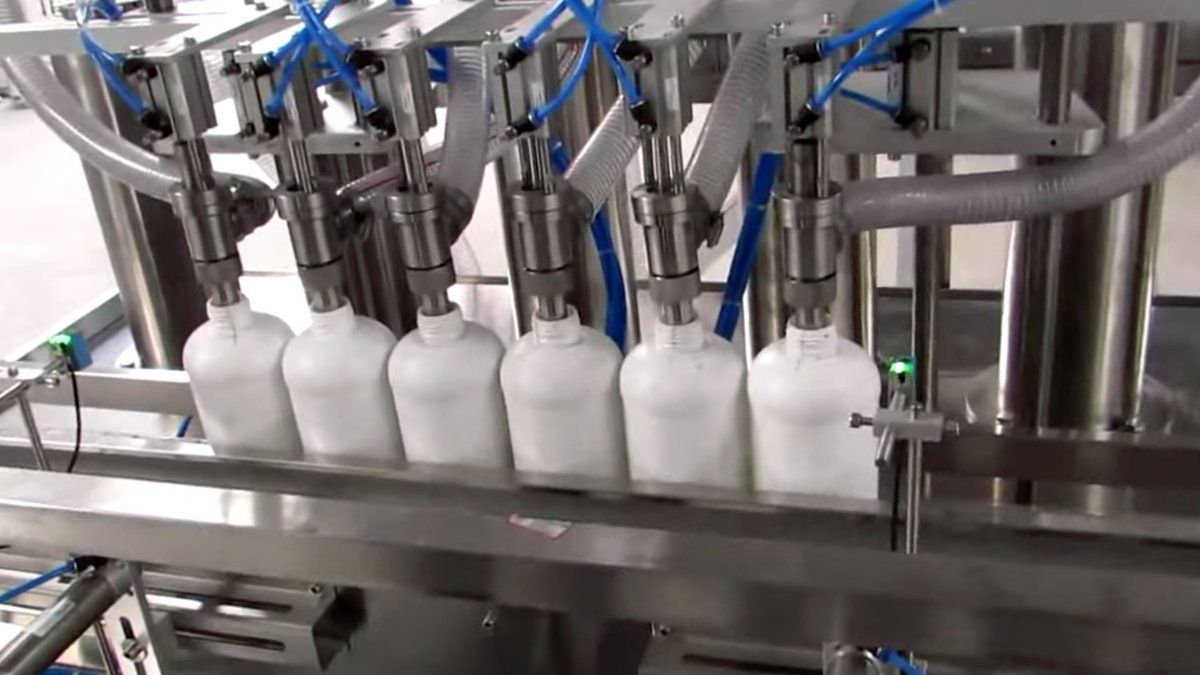
Automated multi-head liquid detergent filling and bottle capping conveyor line in a manufacturing plant
Chemical application profile

Liquid Detergent Manufacturing

Commercial liquid laundry detergents, liquid dishwashing soaps, and hard-surface cleaners in Kenya demand precise stoichiometric neutralization, micellar clarity, and electrolyte viscosity control. KIKI'S supplies primary anionic surfactants (SLES 70%, LABSA 96%), alkalis, and foam builders across East Africa.

Target SectorsIndustrial Cleaning & Hygiene Chemicals Supplier in Kenya · Chemical Manufacturing & Toll Blending Raw Materials Kenya · Industrial Chemicals for Manufacturing Plants in Kenya
Packaging25kg Bags · 200L Drums · IBC Tankers · Bulk Delivery
DocumentationBatch COA, TDS & SDS Available on Request

Quick Answer — Liquid Detergent Manufacturing

For liquid detergent manufacturing applications, KIKI'S Industrial Chemicals supplies documented industrial-grade raw materials and specialty formulation chemicals. We provide consistent chemical inputs and technical documentation to commercial operators across Kenya and the East African market.

Liquid detergent manufacturing involves neutralizing organic sulfonic acids, incorporating secondary ethoxylated surfactants, and titrating electrolyte thickeners into homogeneous liquid cleaning products.

Key Facts

  • •Application: Liquid Detergent Manufacturing
  • •Commercial Supply: Industrial chemical grades with full TDS and SDS documentation
  • •Regional Distribution: Dispatched from Nairobi to production plants across Kenya and East Africa
  • •Procurement Options: Commercial bags, drums, IBC totes, and scheduled delivery agreements

Primary Use Cases

Manufacturing commercial liquid laundry detergents and cold-water washing liquidsCompounding concentrated grease-cutting liquid hand dishwashing soapsProduction of commercial hard-surface and industrial floor cleaning liquidsFormulating high-foaming vehicle wash shampoos and fleet washing concentrates

Technical Process

Micellar Thermodynamics and Active Matter Optimization

The commercial transition from traditional laundry bar soaps to liquid detergents is rapidly accelerating across East Africa. Liquid detergents offer superior cold-water dissolution, leaves zero insoluble chalky residue on fabrics, and integrates seamlessly into automatic washing machines.

A robust commercial liquid detergent formulation balances multiple surfactant chemistries. The primary cleaning engine is Linear Alkylbenzene Sulfonic Acid (LABSA 96%), neutralized with caustic soda (NaOH) to yield sodium alkylbenzene sulfonate. To mitigate skin harshness and provide rapid foam flash, Sodium Lauryl Ether Sulfate (SLES 70%) is incorporated alongside non-ionic foam stabilizers (CDEA 86%).

Electrolyte Thickening, Preservation and Optical Brilliance

Unlike hand dishwashing liquids that rely solely on salt viscosity curves, liquid laundry detergents require advanced builder systems. Sodium Citrate or EDTA chelants sequester calcium ions in hard borehole wash water, while optical brighteners (stilbene derivatives) absorb invisible UV radiation and re-emit blue light, masking fabric yellowing. Preservative systems (isothiazolinones) prevent bacterial contamination in tropical warehouse conditions.

Automated multi-head liquid detergent filling and bottle capping conveyor line in a manufacturing plant

SLES 70%, cocamidopropyl betaine, sodium chloride, optical brighteners, and preservatives for liquid dishwash and laundry detergents.

Standard Application Process

  1. 1

    Treated Water Charging & Chelating

    Charging soft demineralized water and dissolving sodium citrate or EDTA to sequester hardness minerals.

  2. 2

    Caustic Soda Neutralization of LABSA

    Neutralizing LABSA 96% with pre-dissolved caustic soda under continuous cooling to maintain batch <50°C.

  3. 3

    SLES & Secondary Booster Dissolution

    Blending pre-warmed SLES 70% and Cocamide DEA 86% under gentle agitation to prevent excessive aeration.

  4. 4

    Viscosity Adjustment & Salt Titration

    Titrating high-purity vacuum salt brine to cross micellar entanglement and achieve 2,000–3,500 cPs viscosity.

  5. 5

    Brighteners, Dye & In-Can Preservation

    Adding optical brightener, pH-stable dye, fragrance, and broad-spectrum preservative before settling and bottling.

Recommended Chemicals for Liquid Detergent Manufacturing

Showing 1–3 of 3 catalogued products

Filter Full Catalogue (3) →
Surfactants & Detergent Chemicals
Acid Thickerner commercial packaging

Acid Thickerner (Industrial Grade)

Acid Thickerner supplied by KIKI'S Industrial Chemicals in 45kg Drum for industrial, manufacturing, and commercial…

Used for: Liquid Detergent Manufacturing · Detergent & Soap Manufacturing
45Kg Drum (Origin: India)

Industrial Grade · Liquid

View Product
Surfactants & Detergent Chemicals
Cocodiethanolamide 86% (CDEA) commercial packaging

Cocodiethanolamide 86% (CDEA) (Commercial Surfactant Grade)

Cocodiethanolamide 86% (CDEA) supplied by KIKI'S Industrial Chemicals in 200kg plastic drum for industrial,…

Used for: Foam Booster & Viscosity Builder · Liquid Detergent Manufacturing
200Kg Plastic Drum (Origin: Malaysia)

CAS 68603-42-9 · Commercial Surfactant Grade · Liquid

View Product
Surfactants & Detergent Chemicals
Sulphonic Acid / LABSA 90% (Detergent / Industrial Surfactant Grade, Viscous Brown Liquid) in commercial industrial packaging

LABSA 90% (Sulphonic Acid) for Liquid Soap & Detergent Making

Premium Linear Alkylbenzene Sulphonic Acid (LABSA 90%) anionic surfactant for liquid detergent, washing powder, and…

Used for: Liquid Detergent Manufacturing · Anionic Surfactant Formulation
215kg Blue HDPE Plastic Drum1,050kg IBC Tote

CAS 27176-87-0 · Industrial Grade · Liquid

View Product

Key Performance Advantages

  • ✓
    Complete Grease & Oily Stain Removal

    Synergistic sulfonate-ethoxysulfate matrix penetrates deep into fabric fibers to break down stubborn stains.

  • ✓
    Instant Cold-Water Dissolution

    Liquid format dissolves immediately in cold water, leaving zero white residue on dark fabrics.

  • ✓
    Crystal Clarity & Phase Stability

    Controlled neutralization prevents phase separation, sediment drop-out, or cloudiness across seasons.

  • ✓
    High Dilution Economics for Blenders

    Concentrated active bases allow blenders to produce high-margin retail and commercial products.

Key Industrial Use Cases

Commercial liquid laundry detergent and automated machine wash compoundingManual liquid dishwashing soap and grease-cutting kitchen cleaner manufacturingHeavy-duty industrial floor scrubbing liquids and degreasing concentratesAutomotive fleet wash shampoos and high-foaming snow foam concentrates

COMMERCIAL & TECHNICAL GUIDANCE

FAQs — Liquid Detergent Manufacturing

Technical and process guidance for liquid detergent manufacturing in Kenya and East Africa.

Commercial economy liquid detergents typically contain 10% to 14% total active surfactant matter. Premium heavy-duty liquid detergents formulate between 18% and 25% active matter, incorporating optical brighteners and fabric softeners.